Inside opening width and depth
Measure the clear mouth at several positions and note taper, bowing, mould seams or damage instead of relying on outside dimensions.
 EazyMake 3DUseful parts. Made easy.
Editable push-fit lid template
This starter fits an 84 × 56 mm inside opening with 5 mm rounded corners. A 0.20 mm per-side allowance creates an 83.6 × 55.6 mm plug beneath a 92 × 64 mm finger flange, with short calibration coupons before the full lid.
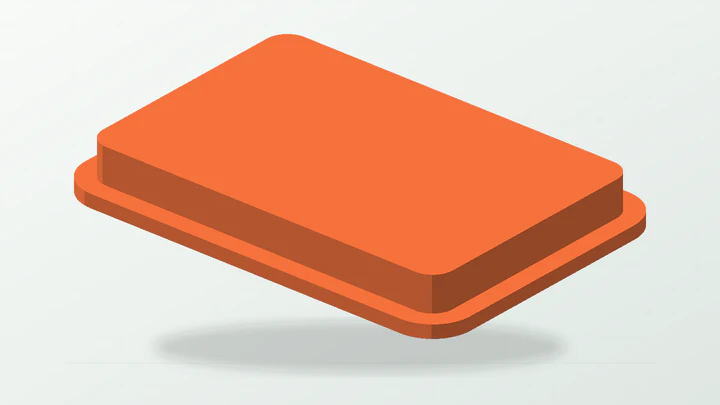
A measured plug-and-flange prototype for a small parts bin—not a seal, latch, retention rating or proof that the original container tolerates the selected fit.
The starter dimensions are there to make the controls understandable. Replace them with evidence from the real part, space and print setup.
Measure the clear mouth at several positions and note taper, bowing, mould seams or damage instead of relying on outside dimensions.
Check the real rounded corners with a radius gauge or fitted references; the plug radius reduces with side clearance.
Measure how far a plug can enter without striking internal ribs, contents, wall taper or other obstructions.
Confirm the flange can rest on the rim and overhang far enough to lift without colliding with handles or neighbouring containers.
These values produce the preview shown above. They remain editable after the template opens in the EazyMake studio.
The generator keeps the important decisions visible and carries one parameter set through geometry, inspection, calibration and export.
Record width, depth and corner radius where the plug will actually enter, including any taper or distortion along the engagement depth.
Decide whether the lid should locate, slide or push snugly, then choose a per-side starting clearance without calling it retention.
Adjust entry depth, overhang and thickness while confirming internal obstructions and external finger access.
Push the tighter, selected and looser trials into the real opening and record the tightest one that seats without forcing.
Print flange-down, inspect the first layer and vertical plug walls, then verify removal and container condition after cooling and repeated trials.
Answers specific to this starter and the measurements it exposes.
The generator subtracts the 0.20 mm side clearance from both sides of the 84 × 56 mm opening, reducing each complete dimension by 0.40 mm.
For the rectangular profile, the same 0.20 mm side clearance is removed from the 5 mm inside corner radius, leaving a 4.8 mm plug radius.
No. Plug fit does not establish a sealing line, material compatibility, leakage performance or retention under pressure or movement.
Treat it as a starting value only. Re-measure and print a small coupon when the container, material, orientation, printer or profile changes materially.
Use the guide when you need the reasoning, or open another template to see the same measurement-first workflow in a different part family.
Open the real generator, replace the example dimensions and keep the calibration result tied to your printer and material.